PET polyester
film tape.
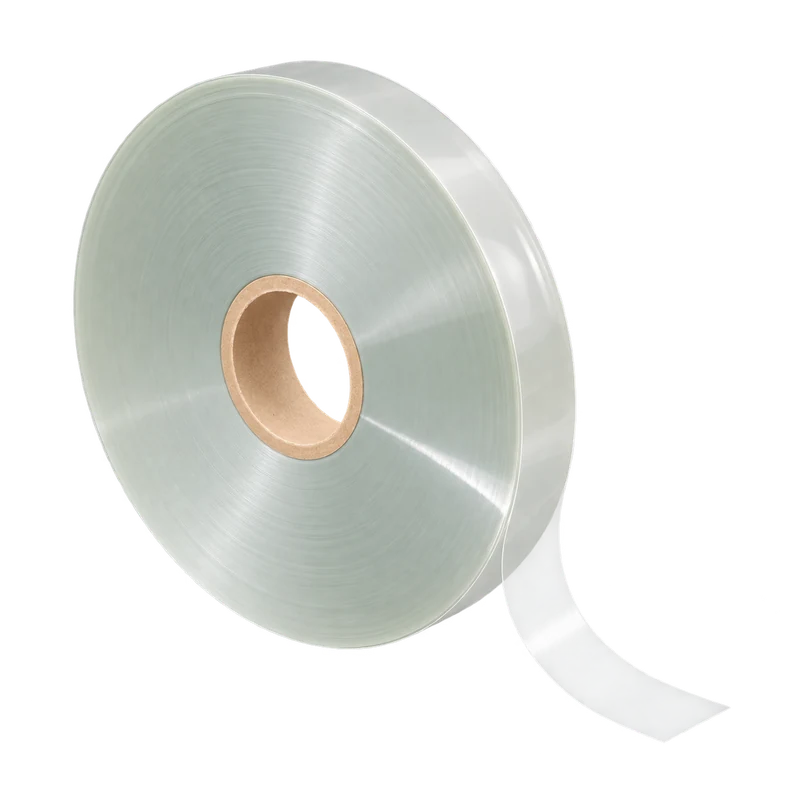
Clear polyester film for cable core binding, layer separation and electrical insulation.
 BIAXIALLY ORIENTED / CLEAR UNCOATED PET
Material construction.
Biaxially oriented, uncoated transparent polyester film. PET provides a smooth, electrically insulating wrap with little addition to cable diameter. Strength and flexibility support controlled taping; low moisture absorption and chemical resistance suit a wide range of cable constructions.
Strong, flexible polyester film
Clear, smooth and non-adhesive
23, 36 and 50 µm
Technical specification.
| Property | Unit | PET23 | PET36 | PET50 |
|---|---|---|---|---|
| Nominal thickness | µm | 23 | 36 | 50 |
| Yield | m²/kg | 31.1 | 19.9 | 14.3 |
| Tensile strength — MD | kg/cm² | 2100 | 2000 | 1900 |
| Tensile strength — TD | kg/cm² | 2200 | 2100 | 2000 |
| Elongation at break — MD | % | 140 | 150 | 170 |
| Elongation at break — TD | % | 135 | 145 | 150 |
| Heat shrinkage — MD* | % | 1.6 | 1.6 | 1.6 |
| Heat shrinkage — TD* | % | 0.2 | 0.2 | 0.2 |
| Coefficient of friction — static | – | 0.40 | 0.42 | 0.42 |
| Coefficient of friction — dynamic | – | 0.35 | 0.32 | 0.32 |
| Surface tension — plain side | dyne/cm | 42 | 42 | 42 |
| Haze | % | 3.0 | 4.2 | 4.2 |
| Light transmission | % | 88 | 88 | 88 |
| Breakdown voltage | kV | 6 | 9 | 11 |
Typical values are guidance, not guaranteed specifications. MD = machine direction; TD = transverse direction. *Heat shrinkage at 150 °C for 30 minutes. Friction values refer to side A / side B. Source units are retained; test methods and tolerances were not specified.
Uncoated PET is non-adhesive and does not provide metallic screening, waterblocking or mica-type fire protection.
Stocked for flexible supply.
Master rolls held in Manchester support fast slitting and spooling to your required widths and winding formats, with smaller minimum order quantities.
Choose pads or traverse spools to suit your line. Custom slit widths, sizes and winding arrangements are available on request.
- Pad slit widths
- PET23: 10–900 mm
PET36 / PET50: 8–900 mm - Spool slit widths
- PET23: 10–60 mm
PET36 / PET50: 5–60 mm - Core IDs
- Pads: 76 or 152 mm
Spools: 76 mm - Maximum OD
- Pads: 550 mm
Spools: 300 mm - Spool core width
- 100–350 mm
Selection and processing.
Select the lowest thickness that meets the required binding, separation and electrical performance. PET23 provides the highest area yield; PET36 and PET50 offer greater film thickness and higher typical breakdown voltage. Confirm suitability in the complete cable and actual processing conditions.
Validate your cable construction.
Match slit width, overlap and tension to the core diameter and equipment. Confirm flat wrapping and stability through extrusion. Breakdown voltage is not a cable working-voltage rating; the shrinkage test temperature is not a continuous-service rating.